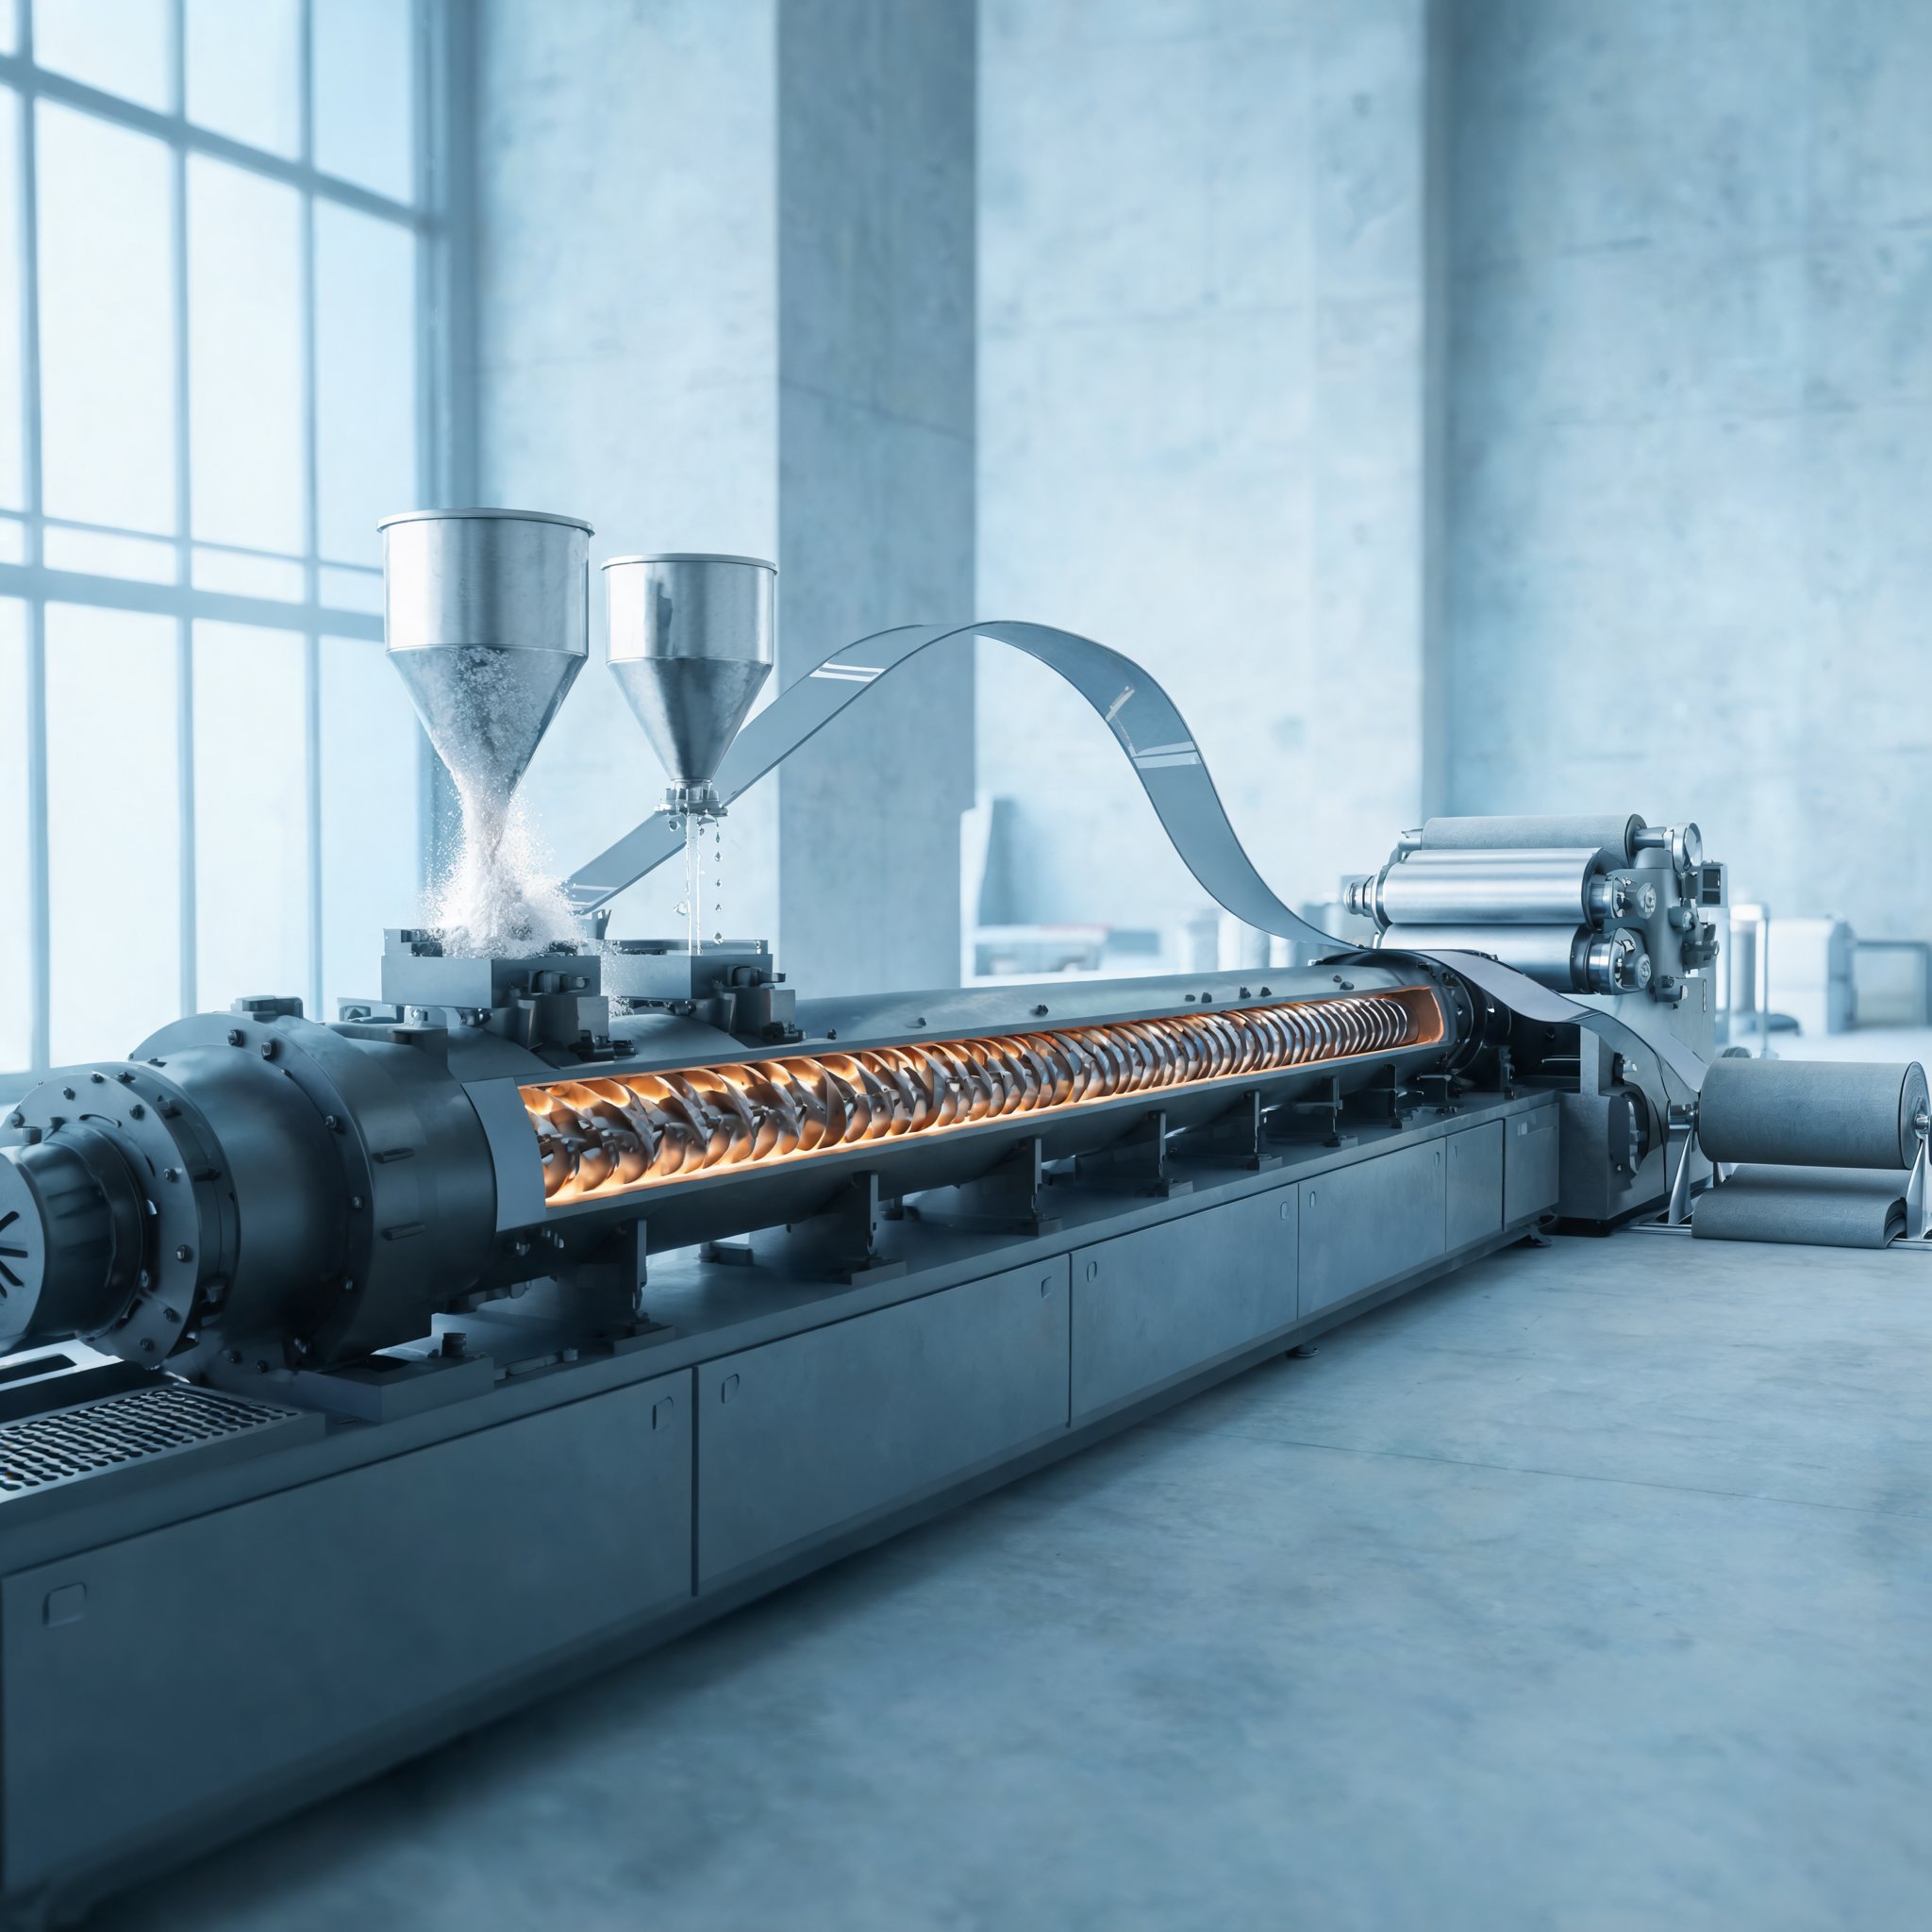
KraussMaffei Extrusion has developed a single-stage extrusion process, marketed as PVC InlineMixing, for the manufacture of PVC roofing membranes. The process replaces the conventional two-stage route in which a dryblend is first prepared in a separate heating-cooling-mixing combination and then plasticized in a twin-screw extruder. According to the company, the continuous alternative cuts energy costs, shortens production time and shortens the payback period on the system.
Removing the dryblend step
In the established two-stage operation, PVC powder, plasticizers, additives and fillers are processed batchwise in a separate hot-cold mixer combination to produce a dryblend. The mixture is cooled, stored intermediately and only then plasticized in a twin-screw extruder and processed into membranes. In the new arrangement, all solid and liquid components are fed directly into the extruder through gravimetric dosing systems, in the quantities the formulation requires, in a continuous flow.
Cost claims: one heat history instead of two
KraussMaffei attributes the savings to several effects. Because no separate heating-cooling-mixing combination is needed, that investment is avoided altogether, and the material has to be heated only once. The company states that energy consumption, and therefore energy cost, falls by up to 75 percent, with the actual figure depending on the formulation, the system parameters and the plant location.
Dropping the standalone mixing stage also shrinks the footprint of the complete line and reduces labor requirements. Maintenance expenditure is described as lower as well, since wear parts for the heating-cooling mixer are no longer required. KraussMaffei frames the combination of reduced capital expenditure and reduced operating costs as the basis for a faster return on investment.
Formulation and color changes during operation
A further stated advantage is production flexibility. Formulation adjustments and color changes can be carried out directly during operation through the integrated control system, which the company says removes the time-consuming preparation and intermediate storage of separate dryblend batches. Christopher Bartel, Head of Sales Flat & Foam at KraussMaffei Extrusion, describes lower production costs, greater flexibility and more efficient manufacturing as a competitive advantage for membrane producers, arguing that they can react faster to new requirements, adjust formulations within the running process and at the same time reduce energy and capital expenditure.
Validation at the Laatzen technology center
The process was developed at the KraussMaffei Extrusion Technology Center in Laatzen and validated using industrial roofing membrane formulations. The trials ran on a co-rotating twin-screw extruder from the ZE 65 BluePower series, equipped with loss-in-weight feeders for all solid components and with multiple liquid feeders for free-flowing formulation ingredients. The ZE BluePower series has a Da/Di ratio of 1.65; the company says the combination of high torque and large free volume opens a wide process window for different formulations.
The tests, according to KraussMaffei, confirmed high gelation levels of the PVC and high product quality, with mechanical properties and weldability of the membranes meeting industrial requirements across several formulations. Bartel says the results show the potential of PVC InlineMixing for industrial roofing membrane production, and that the technology center works with customers to test their own formulations under production-relevant conditions and to optimize the process as a basis for industrial implementation.
First industrial line in operation
The process is already running in an industrial production line for PVC roofing membranes. That reference plant reaches a total throughput of 1,800 kg/h using two extruders and two calenders, with PVC, additives and fillers as well as the resulting edge trimmings processed continuously and directly into finished membranes.